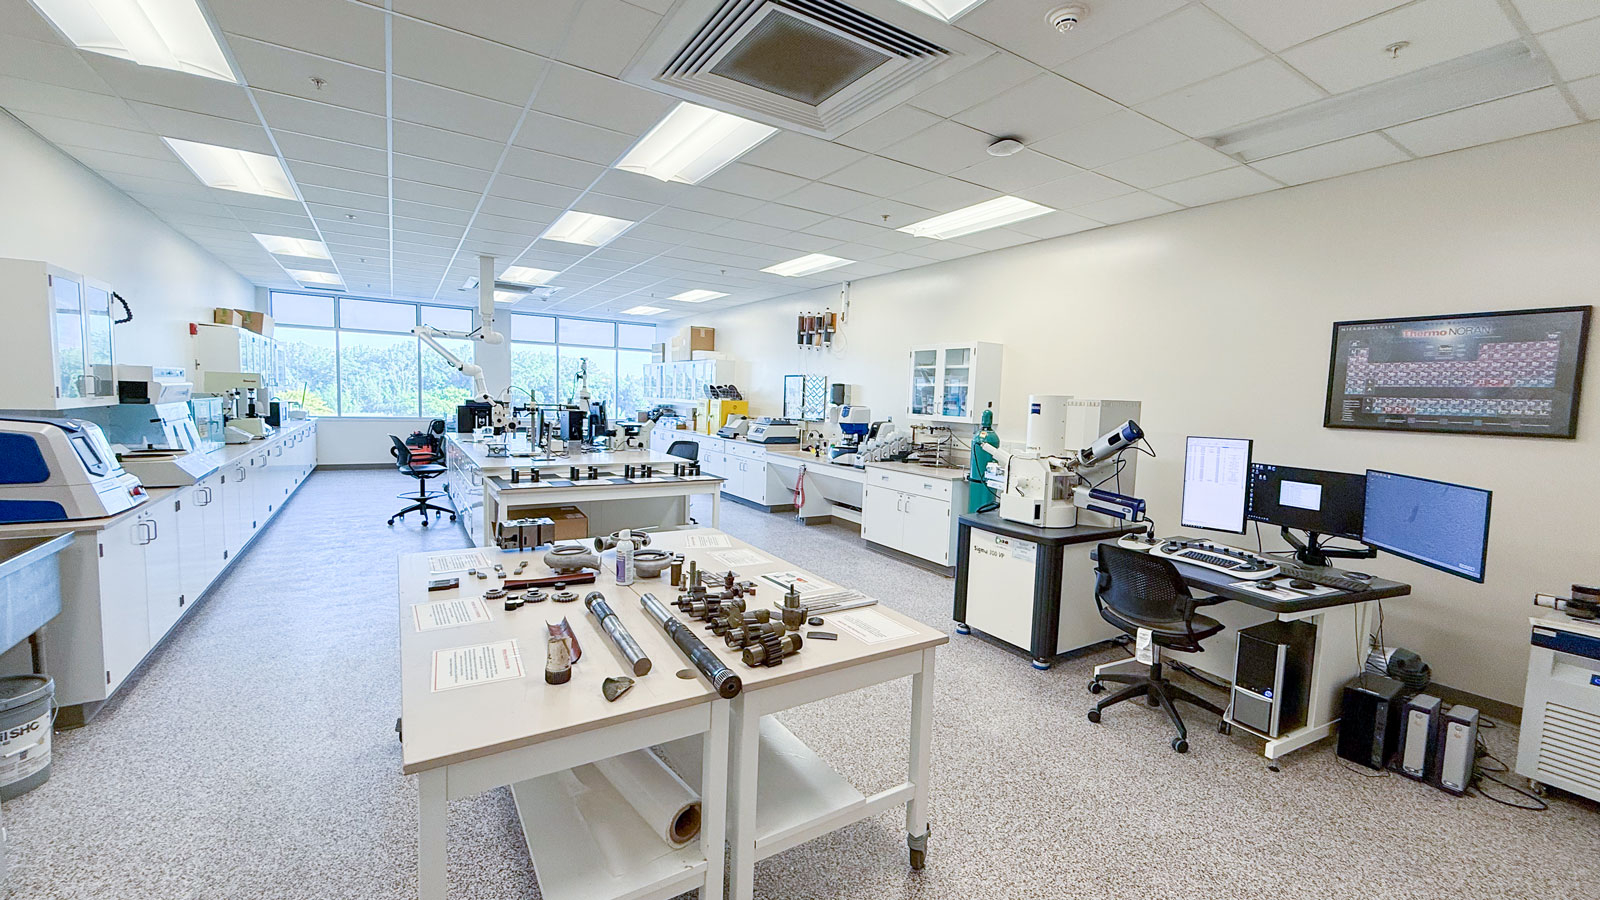
The smell of warm epoxy resin and uncured carbon prepreg is unmistakable. Walk onto the shop floor of any advanced aerospace tier-one supplier or high-performance automotive workshop today, and you will see a quiet industrial revolution unfolding. Engineers are no longer merely guessing how a 32-ply laminate will behave under dynamic thermal loads; they are watching real-time fiber steering data stream directly from automated fiber placement (AFP) heads straight into cloud-hosted simulation hubs.
Yet, for all our sophisticated finite element analysis (FEA) and machine learning micro-structure segmentation frameworks, the shop floor remains wonderfully unforgiving. A single degree Celsius deviation in an autoclave cure cycle or a microscopic void near a primary load-bearing radius can still turn a million-dollar structural wing spar into scrap metal. The gap between what a CAD workstation says is possible and what an autoclave actually delivers is where engineering mastery is truly forged.
The maturation of advanced materials has shifted from raw innovation to disciplined execution. Across sectors ranging from hydrogen storage infrastructure to high-performance electric drivetrains and the Hi-Rate Composite Aircraft Manufacturing (HiCAM) initiatives led by NASA’s consortium partners, the mandate is clear: scale production without sacrificing structural integrity. Practitioners who have spent decades wrestling with ply wrinkling, residual thermal stresses, and resin starvation are rewriting the playbooks, trading theoretical perfection for resilient, field-tested reality.
The Evolution of Structural Mechanics and Material Science on the Shop Floor
Advanced composite design begins long before any material touches a mold. It starts with an intimate understanding of anisotropic behavior—the reality that carbon fiber, glass, and aramid systems are astonishingly strong in the direction of the fibers, and deceptively vulnerable everywhere else. Master practitioners have learned to respect the stiffness matrix rather than fight it, designing ply sequences that account for interlaminar shear stresses before a single FEA mesh is generated.
Material science has evolved past basic unidirectional tapes and plain weaves. Today’s engineers routinely integrate multi-scale reinforcement architectures, hybrid carbon-basalt systems, and toughened epoxy matrices designed to arrest micro-cracking under cyclic fatigue. The integration of artificial intelligence-enabled material design—such as mamba-architecture frameworks and advanced semantic segmentation of scanning electron microscope (SEM) images—allows teams to predict microstructure anomalies before manufacturing even begins.
Despite these digital leaps, the fundamental physics of consolidation remain absolute. Every ply drop, every boundary steering radius, and every tool-part thermal expansion mismatch introduces residual stresses that must be calculated and neutralized. Practitioners emphasize that successful design requires treating the manufacturing method and the structural geometry as a single, inseparable equation. If you design a geometry your autoclave or out-of-autoclave (OOA) vacuum bag cannot consolidate uniformly, you have designed a failure.
Bridging the Chasm Between Digital Simulation and Physical Autoclave Reality
One of the most persistent bottlenecks in composite manufacturing is the discrepancy between virtual prototyping and physical execution. Modern software environments hosted on platforms like cdmHUB allow engineers to simulate resin transfer molding (RTM) and cure kinetics with breathtaking visual fidelity. However, simulation software often assumes ideal boundary conditions that rarely exist on a cluttered, temperature-fluctuating factory floor.
Thermal lag is a classic culprit. A thick monolithic laminate might read 180 degrees Celsius on the surface thermocouple, while the core sits twenty degrees lower, leading to incomplete cross-linking and compromised glass transition temperatures ($T_g$). Experienced tooling engineers counter this by embedding distributed fiber-optic sensors directly into Invar or carbon-composite tooling, giving them real-time visibility into internal thermal gradients throughout the cure cycle.
Furthermore, out-of-autoclave processes have forced a radical rethinking of porosity control. Without external atmospheric pressure clamping down on the laminate, OOA prepregs rely heavily on engineered vacuum channels and precise bleed-off schedules to evacuate entrapped air and volatiles. Practitioners have learned that minor deviations in vacuum bagging technique—a slightly wrinkled breather cloth or a poorly sealed tacky tape corner—can ruin an entire part. Bridging the digital-physical divide means building empirical safety margins directly into your numerical models, accounting for human variability and equipment drift.
Step-by-Step Implementation Framework for High-Reliability Composite Production
Transitioning a composite component from a prototype concept to a high-rate production environment requires rigorous adherence to standardized, repeatable workflows. Drawing from industrial consensus and consortium best practices, the following phased framework ensures structural reliability and process repeatability.
- Step 1 (Parametric Material Characterization): Conduct rigorous coupon-level testing for every new batch of prepreg or resin system, measuring fiber volume fraction, void content via acid digestion or microscopic imaging, and baseline mechanical properties under varying environmental conditions.
- Step 2 (Integrated DFM and Tooling Design): Co-develop the component geometry and tool design simultaneously, factoring in coefficient of thermal expansion (CTE) mismatches to ensure the part releases cleanly and maintains dimensional tolerance upon cooling.
- Step 3 (Automated Deposition and Ply Placement): Utilize automated fiber placement (AFP) or automated tape laying (ATL) systems with real-time laser inspection heads to monitor gap, overlap, and steering angle tolerances down to sub-millimeter thresholds.
- Step 4 (Controlled Consolidation and Cure Monitoring): Execute vacuum bagging and autoclave or OOA cure cycles guided by embedded dielectrics or fiber-optic thermal sensors, adjusting ramp rates dynamically to eliminate exothermic spikes and residual stress.
- Step 5 (Non-Destructive Evaluation and Data Logging): Implement advanced non-destructive evaluation (NDE) protocols—including phased array ultrasonic testing (UT) and flash thermography—while securely logging all processing parameters into a centralized manufacturing execution system (MES) for total traceability.
Navigating Critical Pitfalls and Field-Tested Workarounds on the Production Line
Even with state-of-the-art equipment, composite manufacturing is fraught with subtle failure modes that can halt production lines. Recognizing these hazards early separates amateur operations from world-class manufacturing facilities.
- Pitfall 1 (Bridging and Radius Thinning): Forcing stiff prepreg plies into sharp internal tool radii creates severe bridging, leaving voids and resin-rich pockets that act as crack initiation sites. Workaround: Implement radius fillers (noodle charges) made of compatible unidirectional tow and use radius compaction rollers during hand lay-up or program AFP paths with controlled compaction pressure ramps.
- Pitfall 2 (Exothermic Runaway in Thick Laminates): Thick structural sections can experience uncontrolled exothermic reactions during curing, causing matrix degradation and micro-cracking. Workaround: Program multi-plateau cure cycles with extended dwell periods at lower intermediate temperatures to allow heat dissipation before final ramp-up.
- Pitfall 3 (Fiber Waviness and Wrinkling): Manual handling and aggressive stretching during drape-forming often introduce microscopic fiber waviness, drastically reducing compressive strength. Workaround: Utilize laser projection systems to guide ply placement and employ automated darting and cutting patterns derived from kinematic drape simulation software.
- Pitfall 4 (Moisture Ingress in Honeycomb Sandwich Panels): Trapped moisture inside core cells expands during high-altitude thermal cycling or autoclave curing, causing catastrophic face-sheet debonding. Workaround: Implement rigorous environmental conditioning of core materials prior to bonding and utilize perforated micro-venting septa combined with rigorous edge-sealing protocols.
- Pitfall 5 (Spring-In and Dimensional Distortion): Unsymmetric layups and anisotropic shrinkage cause angle components to spring-in upon tool removal, failing tight assembly tolerances. Workaround: Apply numerical spring-in compensation algorithms to the master tool geometry, effectively over-bending the mold to counteract predictable thermal spring-in.
Balancing Performance, Automation, and Sustainable Lifecycle Engineering
The modern composites industry faces an inescapable paradox: the very materials that make aircraft lighter and electric vehicles more efficient are notoriously difficult to recycle. Thermoset epoxies form permanent chemical cross-links that resist melting, traditionally condemning scrap prepreg and end-of-life structures to landfills. However, the regulatory and corporate landscape is shifting decisively toward circular economy principles.
Practitioners are increasingly turning to recyclable thermoplastic matrices—such as polyetheretherketone (PEEK) and reactive polyamides—which allow components to be reheated, reshaped, and welded at end-of-life. Furthermore, industrial recycling consortia are perfecting mechanical and chemical recycling routes to reclaim high-grade carbon fibers from manufacturing scrap, repurposing them into non-structural automotive panels or chopped molding compounds.
Automation plays a pivotal role in this sustainability drive. Automated cutting tables and near-net-shape preform manufacturing drastically reduce raw material waste, which historically saw up to thirty percent of expensive carbon fabric trimmed away and discarded. By coupling automation with intelligent nesting software and bio-derived resin systems, manufacturers are proving that high structural performance and environmental stewardship are no longer mutually exclusive.
Strategic Frameworks for Scaling Composite Operations and Workforce Competency
Mastering composite design and manufacturing ultimately relies on human expertise. No automated AFP machine or AI simulation tool can replace a skilled technician who senses a subtle tackiness anomaly in a roll of prepreg or an engineer who understands why a specific tool release agent is causing surface pinholes. Building a resilient manufacturing operation requires intentional investment in both hardware and human capital.
Organizations must foster a culture of cross-disciplinary collaboration where materials scientists, structural analysts, and shop-floor technicians share insights seamlessly. Too often, design engineers operate in a vacuum, handing off CAD models to manufacturing teams without understanding the physical constraints of ply draping or autoclave loading. Establishing regular design-for-manufacturing (DFM) reviews bridges this cultural divide.
Training programs must also evolve to reflect contemporary digital realities. Technicians need hands-on exposure to cloud-based simulation tools, digital twin environments, and advanced NDE interpretation. By upskilling workforce competencies alongside technological adoption, companies create an agile manufacturing ecosystem capable of pivoting smoothly from low-volume aerospace prototypes to high-rate automotive production runs.
The journey from raw carbon tow to a flying structural component is a masterclass in disciplined execution. We have moved past the era where advanced composites were treated as exotic novelties; they are now the foundational backbone of clean energy infrastructure, aerospace innovation, and high-performance transportation. Yet, the core truth remains unchanged: mastery is earned on the shop floor through meticulous attention to detail, profound respect for material physics, and a relentless commitment to continuous improvement.
As the industry looks toward increasingly ambitious automation milestones, distributed cloud manufacturing, and fully circular material lifecycles, the practitioners who thrive will be those who balance digital ambition with tactile intuition. Embrace the complexities of your materials, respect the boundaries of your manufacturing processes, and never stop learning from the anomalies that happen when resin meets heat and pressure. The future of engineering is composite, and it is being built one meticulously cured ply at a time.